



Conveying Units
Pneumatic Diverter Valve
The pneumatic diverter valve switches product flow between two pipelines in seconds, actuated by compressed air and controlled from the panel.
The diverter valve directs product arriving from one inlet to either of two outlets. The blade inside the body is moved by a pneumatic cylinder and its end positions are reported to the panel by sensors.
Sealing faces prevent product from leaking into the line that is not selected, so switching between different flours or different bins carries no risk of mixing.
The body and blade are made of wear-resistant sheet, and the maintenance cover comes off for access to the internal parts. A stainless body is available depending on the product.
Key features
- Pneumatic actuation switches direction in seconds
- Position sensors reported to the panel
- Sealing faces that eliminate the risk of mixing
- Wear-resistant body and blade
- Stainless body option
Applications
- Flour and semolina distribution lines
- Silo filling and route selection
- Automatic blending and dosing systems
How it works
Working principle
Conveying moves grain and milled products between every stage of the plant with minimal energy and no product damage.
- 1Product enters the boot of the elevator from a conveyor or hopper.
- 2Buckets on an endless belt lift it up the loaded leg and over the head pulley.
- 3Centrifugal force throws the product into the discharge spout, from where screw or chain conveyors and pneumatic lines carry it on.
Technical specifications
Technical data is available on request.
Related machines
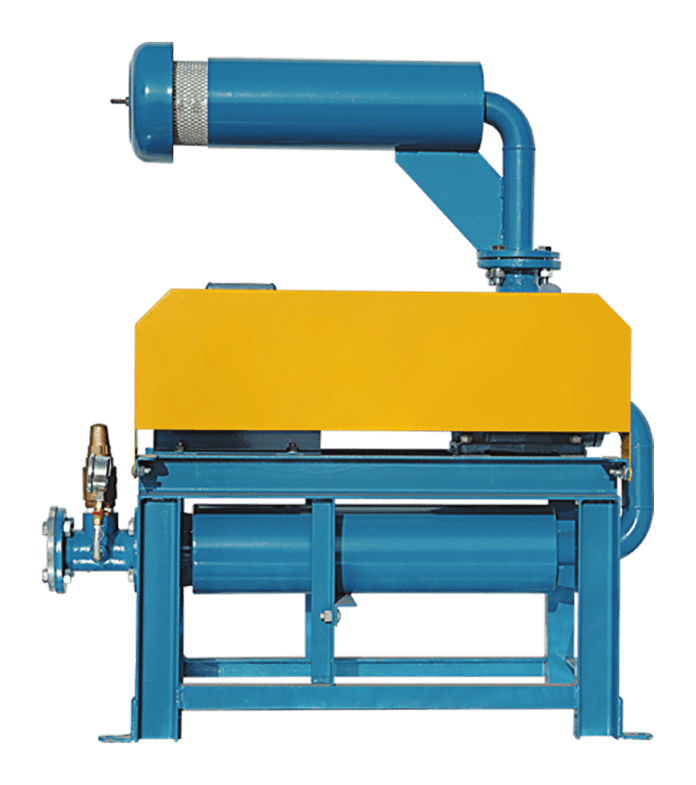
HKBP
Blower Pump
The blower pump is a rotary lobe blower that supplies pressure air to the pneumatic conveying lines for flour and bran, running continuously and quietly.
Explore
HKBHK
Blower Air Lock
The blower air lock is a rotary valve that feeds product into a pressurised pneumatic line while sealing against air loss.
Explore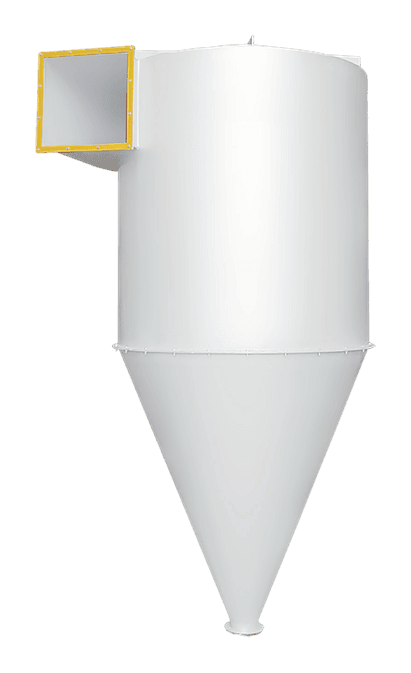
Dust Cyclone
The dust cyclone drops dust and product out of an air stream by centrifugal force, with very low maintenance and no filter media.
Explore