


Elevators, conveyors, air locks and pneumatics that keep product moving
Conveying Units
Bucket elevators, screw and chain conveyors, flour and bran screws, blowers, air locks, pneumatic diverter valves, blending machines, dust aspirators and cyclones move grain and milled products between every stage of the plant with minimal energy and no product damage.
12 machines

How it works
Working principle
Conveying moves grain and milled products between every stage of the plant with minimal energy and no product damage.
- 1Product enters the boot of the elevator from a conveyor or hopper.
- 2Buckets on an endless belt lift it up the loaded leg and over the head pulley.
- 3Centrifugal force throws the product into the discharge spout, from where screw or chain conveyors and pneumatic lines carry it on.
Machines in this category
HKE
Bucket Elevator
The bucket elevator lifts wheat, flour and bran vertically on a belt and bucket assembly, with capacities per product given in the model table.
Explore
HKVH
Screw Conveyor
The screw conveyor moves grain and ground products horizontally or on a slight incline in a trough, with several inlets and outlets possible.
Explore
HKTA
Tube Screw Conveyor
The tube screw conveyor handles inclined and near-vertical transport in a closed tube, giving a completely dust-tight product transfer.
Explore
HKUKV
Flour & Bran Screw Conveyor
The flour and bran screw conveyor is designed to collect fine, powdery flour and light bran from several sifter outlets and move them to packing.
Explore
HKZK
Chain Conveyor
The chain conveyor moves grain and bran gently over long distances with an en-masse drag chain running slowly in a closed trough.
Explore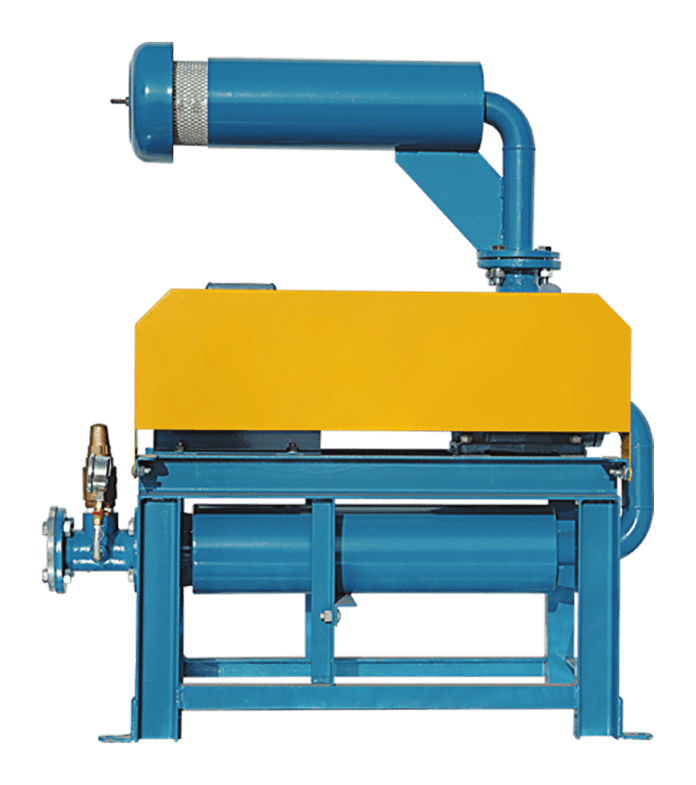
HKBP
Blower Pump
The blower pump is a rotary lobe blower that supplies pressure air to the pneumatic conveying lines for flour and bran, running continuously and quietly.
Explore
Pneumatic Diverter Valve
The pneumatic diverter valve switches product flow between two pipelines in seconds, actuated by compressed air and controlled from the panel.
Explore
HKBHK
Blower Air Lock
The blower air lock is a rotary valve that feeds product into a pressurised pneumatic line while sealing against air loss.
Explore
HKAL
Air Lock
The air lock is a rotary valve under cyclones, filters and hoppers that discharges product while maintaining the air seal.
Explore
Blending Machine
The blending machine combines wheat or flours from different bins in set proportions to build a uniform grist or recipe before packing.
Explore
HKDSF
Low-Pressure Fan (Dust Aspirator)
The low-pressure fan draws dust from machines and conveyors and delivers the collected air to a cyclone or filter line.
Explore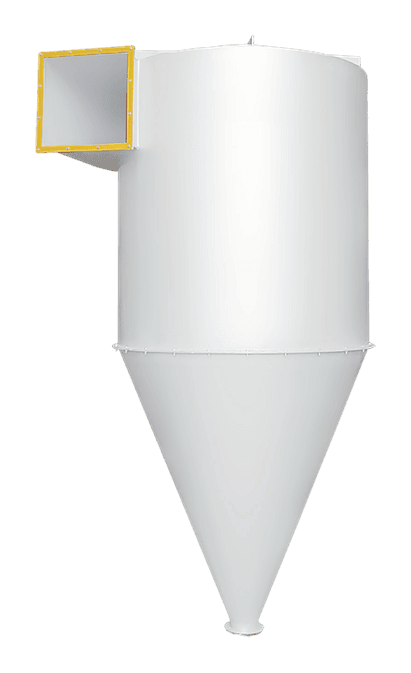
Dust Cyclone
The dust cyclone drops dust and product out of an air stream by centrifugal force, with very low maintenance and no filter media.
Explore
Let's plan your mill together
Tell us your product, capacity and site. Our engineers reply with a configuration and a quotation, usually within two working days.